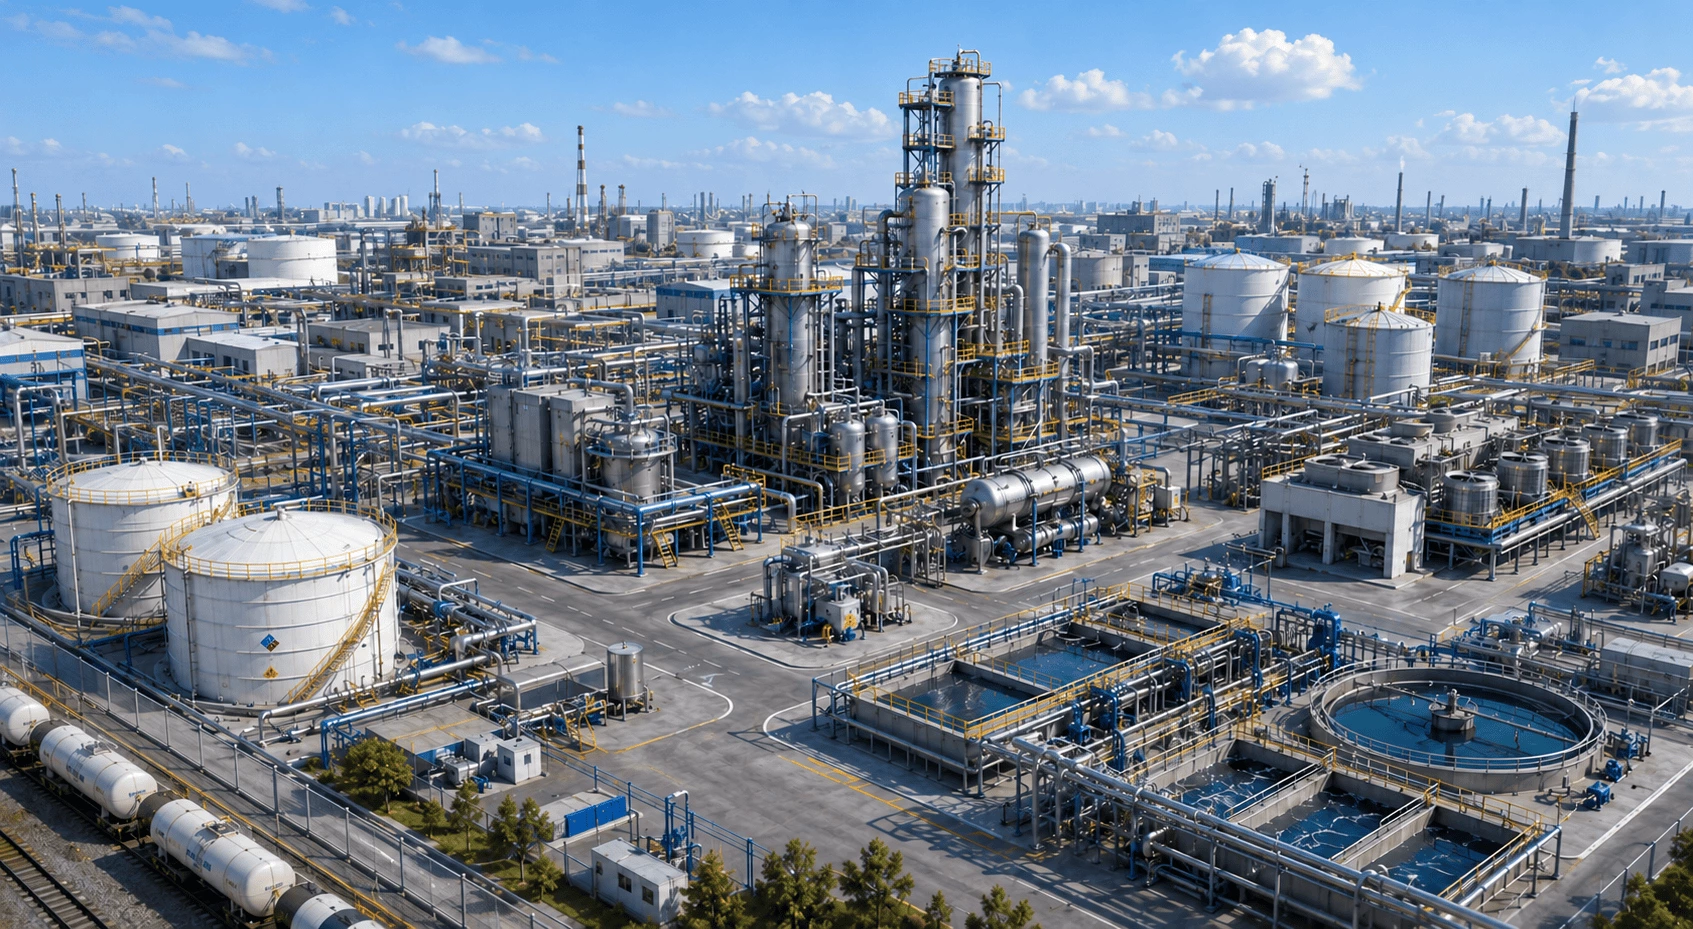
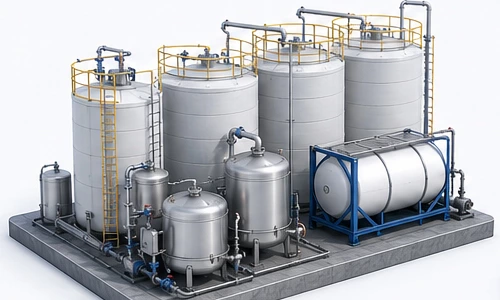
Safely store liquid chemicals, solvents, acids, alkalis, and bulk raw materials before production while ensuring accurate inventory management.
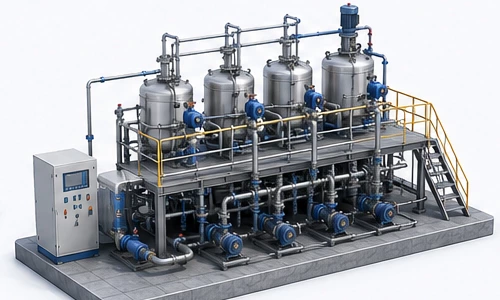
Accurately measure and control the flow of raw materials and additives entering reactors for consistent product quality.
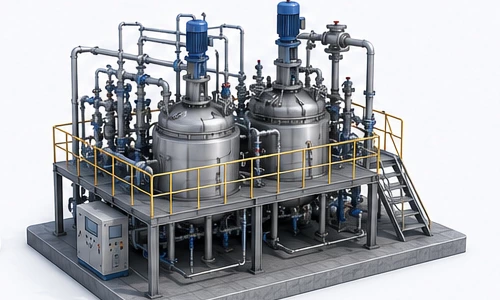
Monitor critical process variables to maintain stable reaction conditions and maximize production efficiency.
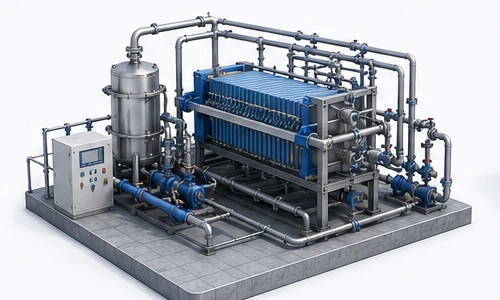
Separate reaction products and remove impurities through filtration, distillation, centrifuges, or evaporation systems.
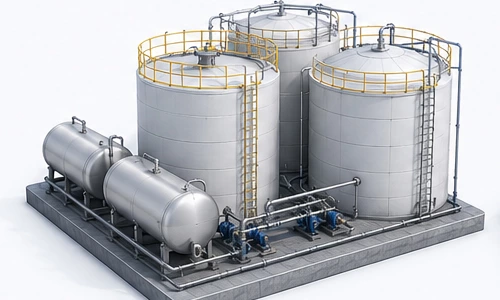
Maintain safe storage and inventory control for finished chemicals before packaging or transportation.
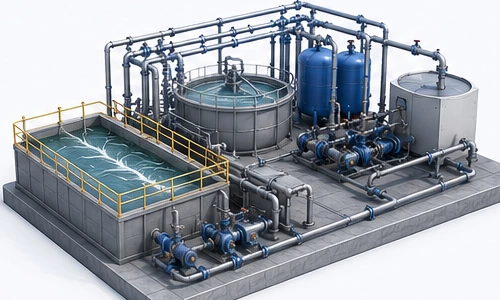
Optimize utility systems and wastewater treatment to improve sustainability and regulatory compliance.
We use cookies to collect information about how you use this site. We use this information to make the website work as well as possible and improve our services.